


PET Bottle Maker Machine Capacity Guide: Matching BPH Output to Your Production Goals
 Oct 12, 2026|
 View:133
When a beverage or packaging company starts planning a new line, the first question is almost always the same: how many bottles do we need every hour? The answer decides everything — which PET bottle maker machine to buy, how many cavities the molds need, how much floor space is required, and what the line will cost to run. Output is measured in BPH (bottles per hour), and choosing the right BPH range is where most purchase decisions are won or lost. This guide explains, in plain language, what BPH really means, how machine capacity is calculated, and how a manufacturer can match machine output to their actual production goals without overbuying or underbuying.
Key Takeaways
BPH (bottles per hour) is the single most important specification when buying a bottle maker — it must match your daily demand, operating hours, and efficiency.
Real output depends on more than the machine's rated speed: cavity count, bottle size and weight, preform heating capacity, and compressed air supply all play a role.
Small single-cavity machines serve large-format bottles (5–20 L barrels), while standard and high-speed linear machines cover 200 ml–2,000 ml beverage bottles.
Matching capacity means calculating required BPH from your production goal, then adding a practical efficiency margin — typically 80–90% of rated output.
Energy recovery, floor space, mold changeover speed, and after-sales support matter as much as the headline BPH number for total cost of ownership.
What Is a PET Bottle Maker Machine and What Does BPH Mean?
A PET bottle maker machine — also called a PET bottle blowing machine or stretch blow molding machine — turns injection-molded preforms into finished PET bottles. The preform, which looks like a small test tube with a bottle neck, is heated in an infrared oven until the plastic reaches its forming temperature. It is then stretched and inflated by high-pressure air inside a closed mold, producing a bottle with the exact shape of the mold cavity. The process is fast, repeatable, and well suited to water, beverages, edible oil, and other liquid products. Industry background on PET containers — including material properties and recycling — is available from the national association for PET container resources.
BPH stands for bottles per hour, and it is the standard way the industry describes machine output. A machine rated at 12,000 BPH is designed to produce about 12,000 bottles in one hour of continuous operation. BPH is not a theoretical maximum — it is the sustainable production rate under normal operating conditions, and it depends on several variables discussed below. Understanding BPH is the first step to choosing the right machine for a specific production goal.
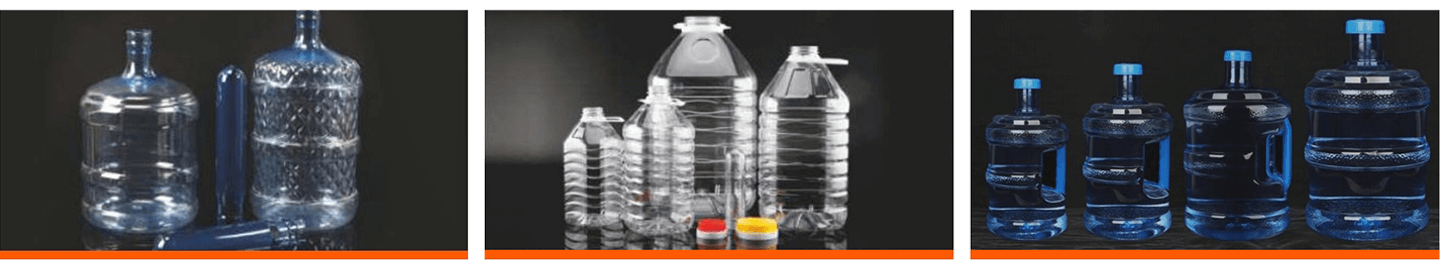
The Real Output Equation: How Capacity Is Actually Calculated
Rated BPH is a useful starting point, but real output is the product of several interacting factors. The basic relationship is simple:
Output (BPH) ≈ number of mold cavities × cycles per hour
Every time the machine closes, each cavity produces one bottle. A single-cavity machine produces one bottle per cycle; a double-cavity machine produces two, and so on. But the machine can only cycle as fast as the slowest step in the process allows. The practical factors that limit throughput include:
Bottle size and preform weight: larger bottles need more material, more heating, and more cooling time. A machine rated 12,000 BPH on a 500 ml bottle will produce fewer large-format bottles per hour.
Preform oven capacity: the infrared oven must heat preforms to the correct temperature profile. If the oven cannot keep up with the blowing station, output drops regardless of the rated speed.
Compressed air supply: stretching and blowing consume high-pressure air (typically up to 40 bar). An undersized compressor is a common cause of output shortfalls.
Cycle time and cooling: thicker, heavier bottles need longer cooling inside the mold before they can be ejected without deformation.
Changeover and maintenance time: mold changes, cleaning, and routine stops reduce the number of productive hours in a shift.
Peer-reviewed research on preform heating and stretch blow molding shows how sensitive bottle quality and process stability are to these parameters — another reason rated output should be treated as a planning figure, not a guarantee. Modern machines address the process side with servo-driven stretching, closed-loop heating, and peer-reviewed research on PET container quality underlines why consistent forming conditions matter for stress-crack resistance and clarity.
BPH Ranges Across Machine Types: What to Expect
PET bottle making machines come in three broad families, and each has its own BPH territory. The table below summarizes typical expectations.
| Machine Type | Typical BPH | Typical Bottle Size | Best Suited For |
|---|---|---|---|
| Single-cavity big-barrel machine | 800–1,500 BPH | 5 L–20 L barrels | Water barrels, edible oil containers, large jugs |
| Standard linear machine | 12,000–18,000 BPH | 200 ml–1,500 ml | Mid-size water and beverage plants |
| High-speed linear combiblock | 24,000–27,000+ BPH | 200 ml–2,000 ml | Large beverage facilities, integrated fill-cap lines |
| Large rotary systems | Higher than linear (commonly above 40,000 BPH on small water formats) | Small-format water bottles | Very large, dedicated single-SKU lines |
There is no "best" type — only the right fit. A plant making 20 L water barrels does not need a 24,000 BPH machine; a plant filling 500 ml water for retail distribution will not be served by a single-cavity barrel machine. The choice follows the production goal.
Matching BPH to Your Production Goals: A Simple Calculation
Selecting the right capacity starts with a simple calculation. The formula is:
Required BPH = daily bottle demand ÷ planned operating hours ÷ efficiency factor
The efficiency factor accounts for stops, changeovers, and normal downtime. A factor of 0.85 (85%) is a common planning assumption. The table below shows three worked examples.
| Scenario | Daily Demand | Operating Hours/Day | Efficiency | Required BPH | Suitable Machine |
|---|---|---|---|---|---|
| Small water plant | 30,000 bottles | 16 h | 85% | ≈ 2,200 BPH | Standard linear machine (with margin) |
| Mid-size beverage plant | 150,000 bottles | 20 h | 85% | ≈ 8,800 BPH | Standard linear 12,000–18,000 BPH |
| Large facility, single SKU | 350,000 bottles | 20 h | 85% | ≈ 20,600 BPH | High-speed linear 24,000–27,000+ BPH |
Notice that the machine's rated BPH should be comfortably above the calculated requirement. A line running at 100% of rated output every day leaves no room for seasonal peaks, new products, or gradual efficiency improvements. Planning with margin also protects the line when the filling and capping equipment run at a different speed — which is why many producers choose combiblock systems that synchronize blowing with filling and capping in one machine, as available on high-speed linear platforms.
Beyond BPH: Cost Factors That Decide the Real Value
Two machines with the same BPH can have very different running costs. Before comparing prices, buyers should check the factors that determine total cost of ownership.
| Cost Factor | What to Check | Typical Impact |
|---|---|---|
| Compressed air consumption | Air recovery or closed-loop recycling systems | Up to 50% lower compressor energy load on well-designed machines |
| Floor space | Linear air-free transfer, integrated combiblock layout | More than 30% less floor space versus traditional conveyor layouts |
| Mold changeover | Quick-lock clamping, rapid-change mandrels | Changeover under 30–45 minutes keeps more hours productive |
| Spare parts and service | Standardized Tier-1 components, global availability | Off-the-shelf parts reduce downtime and avoid vendor lock-in |
| Compliance | CE machinery directives, ISO 9001, food-contact materials | Required for export markets and food-safe production |
For example, a machine with dual-stage pneumatic recovery captures exhaust air from the blowing stages and redirects it to low-pressure actuation loops, cutting compressor energy loads by up to 50% during continuous runs. Over a 20-hour production day, that difference appears directly in the electricity bill. Similar logic applies to U.S. regulations for PET food-contact materials — machines used for beverage packaging must be built and operated with food-contact compliance in mind.
How to Choose a PET Bottle Maker Machine Manufacturer
Choosing the right bottle blowing machine is a long-term investment, and the supplier's engineering depth matters as much as the specification sheet. The checklist below is a practical starting point when comparing proposals.
| Criterion | What to Check | Why It Matters |
|---|---|---|
| Track record | Machines delivered, markets served, references | Field experience predicts real-world reliability |
| Automation platform | Standardized PLC and servo architecture | Determines precision, repeatability, and spare-part availability |
| Mold support | In-house mold design, cavity options, neck finishes | Molds define output, quality, and changeover speed |
| Process engineering | Heating control, stretch profiles, air management | Directly affects bottle quality and energy cost |
| After-sales service | Installation, training, spare parts, maintenance | Downtime costs more than the difference in purchase price |
| Compliance documents | CE, ISO 9001, food-contact certificates | Required for export and food-safe production |
When comparing quotes, ask for the BPH rating at your specific bottle size and preform weight — a number quoted for a 500 ml bottle does not apply to a 2 L bottle. Also ask about cycle time, air consumption, changeover time, and the mold set included in the price. A serious supplier will request your bottle drawing, target output, and filling plan before quoting.
Need a PET Bottle Maker Machine That Matches Your Output?
TENYUE designs linear PET bottle making machines from 12,000 to 27,000+ BPH, plus single-cavity big-barrel machines for 5–20 L containers, with energy recovery, fast changeover, and food-contact compliance. Get a free consultation and a quotation based on your bottle size and daily production goal.
Conclusion
Choosing the right PET bottle maker machine is fundamentally a numbers exercise: daily demand, operating hours, efficiency, bottle size, and the BPH rating that ties them together. Start with the calculation, add a practical margin, and then compare machines on the factors that determine running cost — air consumption, floor space, changeover speed, and service support. A machine that matches the production goal today, with room for tomorrow, is the one that pays for itself. And because every plant is different, the most valuable step is the same for every buyer: talk to the manufacturer with your real numbers, and let them propose the fit.
Frequently Asked Questions
What does BPH mean in a PET bottle maker machine?
BPH stands for bottles per hour — the number of finished bottles the machine can produce in one hour of continuous operation. It is the standard way to compare machine capacity.
How do I calculate the capacity I need?
Divide your daily bottle demand by planned operating hours and an efficiency factor (commonly 0.85). The result is the minimum required BPH; choose a machine rated comfortably above it.
What is the difference between linear and rotary PET bottle machines?
Linear machines move preforms in a straight line and suit 12,000–27,000+ BPH ranges with flexible changeover. Rotary machines rotate continuously and reach higher speeds, mainly on small, dedicated water formats.
How many cavities do I need?
Each cavity produces one bottle per cycle, so more cavities mean higher output. The right number depends on your BPH target and bottle size; mold cost and cooling time also increase with cavity count.
What bottle sizes can a PET bottle machine produce?
Linear beverage machines typically cover 200 ml–2,000 ml bottles, while single-cavity machines handle 5 L–20 L barrels. The practical range depends on the machine platform and mold set.
Why does BPH drop for larger bottles?
Larger bottles use heavier preforms that need more heating and cooling time, so each cycle takes longer. A machine rated on 500 ml bottles will produce fewer 2 L bottles per hour.
How do I choose a PET bottle maker machine manufacturer?
Check track record, automation platform, mold support, process engineering, after-sales service, and compliance documents. Ask for the BPH rating at your bottle size, plus air consumption and changeover time in the quotation.


